
Advanced Humidity Sensor Technologies Strengthen Moisture Control in Semiconductor Manufacturing
Semiconductor manufacturing requires extremely precise control over environmental conditions to maintain product quality, process stability, and production efficiency. Even minor variations in moisture levels can affect sensitive materials, influence chemical reactions, and compromise the performance of semiconductor devices. As chip architectures become increasingly complex, manufacturers are investing in advanced humidity sensor technologies to improve environmental monitoring and moisture management. These technologies provide accurate, continuous measurements that help production teams identify humidity fluctuations before they affect critical manufacturing operations. Their integration into cleanrooms, wafer fabrication facilities, and specialized storage environments is becoming an important part of modern semiconductor process control.
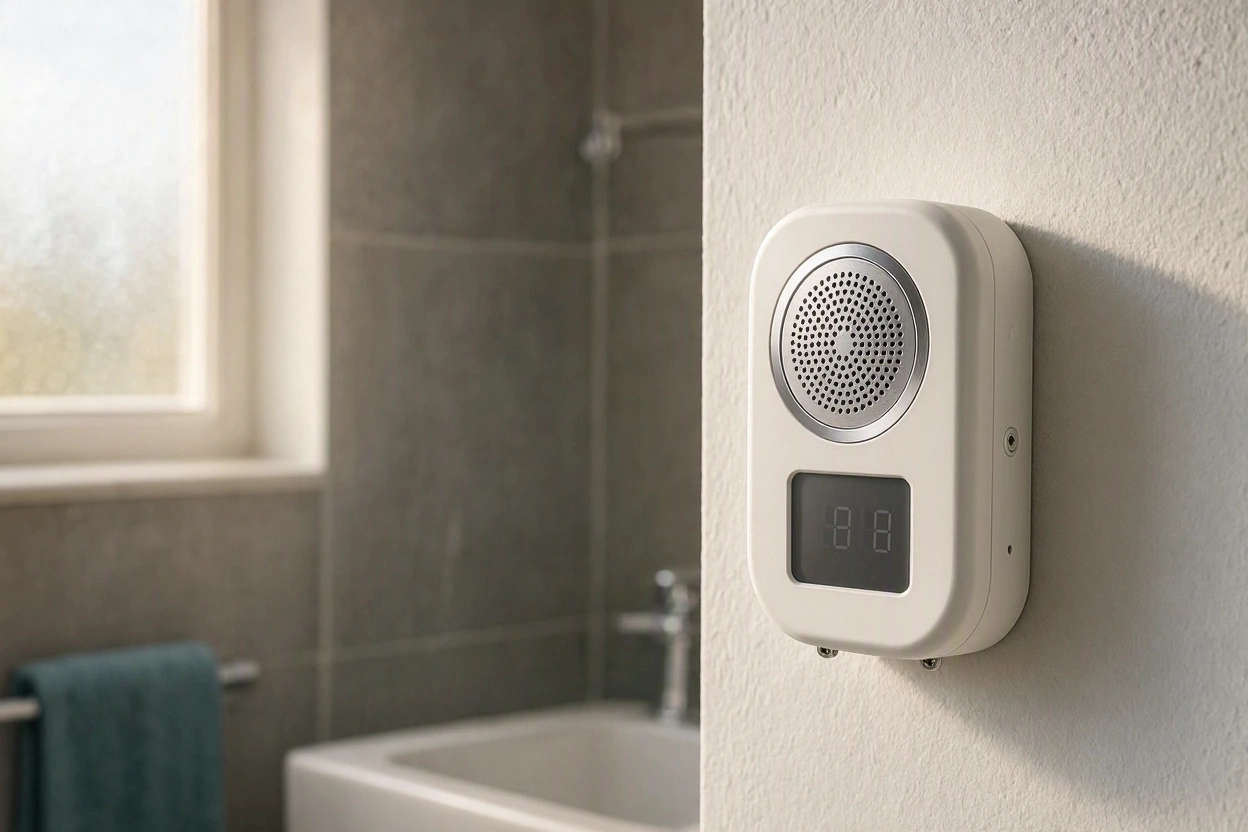
According to Marketsandmarkets, the global humidity sensor market size is projected to grow from USD 3.64 billion in 2026 to USD 5.32 billion by 2032, growing at a CAGR of 6.5% from 2026 to 2032.
Download PDF Brochure @ https://www.marketsandmarkets.com/pdfdownloadNew.asp?id=222120714
The growing demand for high performance chips, advanced packaging, and miniaturized electronic components is increasing the importance of precise humidity monitoring. Semiconductor production involves several moisture sensitive materials, including photoresists, specialty chemicals, substrates, and electronic components. Uncontrolled moisture can contribute to contamination, material degradation, corrosion, and defects during selected manufacturing processes. Advanced humidity sensor technologies help manufacturers maintain stable environmental conditions through reliable measurement, automated monitoring, and integration with facility management systems. By improving visibility into humidity variations, these solutions support more consistent production conditions and help semiconductor facilities strengthen operational reliability.
Importance of Moisture Control in Semiconductor Manufacturing
Moisture control plays a critical role in semiconductor fabrication because different production stages require carefully managed environmental conditions. Photolithography, wafer cleaning, chemical processing, and electronic assembly may each have specific humidity requirements. Excessive moisture can affect material properties, while insufficient humidity may increase electrostatic discharge risks in certain manufacturing environments. These challenges make precise environmental monitoring essential for protecting sensitive wafers and maintaining repeatable production results. Humidity sensor technologies provide the measurement capabilities required to identify deviations and support timely corrective action.
Semiconductor cleanrooms depend on coordinated control of temperature, humidity, air quality, and particulate contamination. Humidity fluctuations can influence static electricity, surface conditions, and the behavior of certain process materials. For example, moisture absorption by hygroscopic materials can change their physical properties and affect handling or processing performance. Reliable sensors help facility operators monitor environmental conditions across different cleanroom zones and identify localized variations that centralized measurements might overlook. This detailed monitoring supports improved process consistency and helps manufacturers maintain environmental specifications throughout production.
Advanced Humidity Sensor Technologies Improve Measurement Accuracy
Modern humidity monitoring solutions use several sensing principles to measure moisture in air and controlled industrial environments. Capacitive sensors measure changes in electrical capacitance associated with moisture absorption in a sensing material. Resistive sensors detect variations in electrical resistance as humidity changes, while advanced thermal conductivity and chilled mirror instruments serve specialized measurement requirements. Each technology offers different advantages in terms of accuracy, response time, operating range, maintenance, and cost. Semiconductor manufacturers select appropriate sensors according to process sensitivity, environmental conditions, and required measurement performance.
Continuous improvements in sensing materials, electronics, and signal processing are strengthening the capabilities of humidity monitoring systems. Advanced humidity sensor technologies can provide more stable measurements, improved temperature compensation, and better resistance to environmental interference. Digital interfaces also simplify communication between sensors, monitoring software, and industrial control platforms. These features help reduce measurement uncertainty and provide operators with more useful information about changing environmental conditions. As a result, manufacturers can make better informed decisions about cleanroom control, equipment operation, and moisture sensitive process management.
Role of Capacitive Sensors in Cleanroom Monitoring
Capacitive humidity sensors are widely used in environmental monitoring because they offer compact designs, practical integration, and continuous measurement capabilities. These sensors typically contain a moisture sensitive dielectric material positioned between conductive elements. When the material absorbs water vapor, its dielectric properties change, producing a measurable variation in capacitance. Electronic circuits convert this variation into a humidity reading that can be transmitted to a monitoring system. Their combination of size, measurement capability, and integration flexibility makes capacitive sensing suitable for many cleanroom and industrial monitoring applications.
In semiconductor facilities, capacitive sensors can support humidity monitoring in cleanrooms, material storage areas, equipment enclosures, and air handling systems. Their readings help operators determine whether environmental conditions remain within established process limits. Proper sensor placement is essential because humidity can vary between different rooms, equipment locations, and air circulation zones. Calibration and maintenance are equally important for ensuring measurement reliability over time. When deployed as part of a comprehensive environmental monitoring strategy, capacitive sensors help semiconductor manufacturers maintain greater control over moisture sensitive operations.
Emerging Sensing Methods Support Specialized Applications
Although capacitive sensors serve many general monitoring needs, some semiconductor applications require more specialized measurement methods. Chilled mirror hygrometers determine dew point by cooling a surface until condensation forms, providing highly accurate measurements in applications where reference level performance is required. Thermal conductivity sensors estimate moisture concentration by measuring changes in the thermal properties of a gas mixture. Certain industrial moisture analyzers also support measurements in process gases and specialized production environments. These instruments can complement conventional humidity sensors where trace moisture detection or specialized gas monitoring is necessary.
The selection of a sensing method depends on the application rather than a single universal performance standard. A cleanroom monitoring system may prioritize dependable relative humidity measurements, while a specialty gas distribution system may require precise trace moisture analysis. Temperature, pressure, chemical exposure, and contamination risks can also influence instrument selection. Manufacturers must evaluate these conditions before choosing equipment for a particular process. Combining complementary measurement technologies can provide better environmental visibility and support more reliable process control across complex semiconductor facilities.
Benefits of Real Time Humidity Monitoring
Real time monitoring enables semiconductor manufacturers to identify environmental deviations as they occur instead of relying exclusively on periodic manual inspections. Connected sensors can continuously transmit measurements to building management systems, environmental monitoring platforms, or manufacturing control software. When readings exceed configured thresholds, the system can generate alerts for facility engineers and process operators. This allows teams to investigate abnormal conditions and take corrective action before environmental instability affects production. The resulting visibility supports faster responses and more consistent control of critical manufacturing environments.
Key operational benefits include:
- Improved process consistency: Continuous measurement helps maintain environmental conditions within defined operating limits.
- Reduced material exposure:Early warnings allow teams to investigate humidity excursions that could affect sensitive materials.
- Better facility efficiency:Integrated monitoring helps operators identify recurring environmental fluctuations and optimize control strategies.
- Enhanced traceability:Digital records support environmental reviews, quality investigations, and internal compliance procedures.
These benefits depend on proper system configuration, reliable sensor placement, regular calibration, and appropriate alarm thresholds. Monitoring alone cannot prevent every manufacturing defect, but it provides essential information for maintaining controlled production conditions.
Integration With Smart Factory Automation
The adoption of smart manufacturing is creating new opportunities for humidity sensor technologies in semiconductor production. Connected sensors can integrate with industrial communication networks, building automation platforms, and centralized environmental monitoring systems. This connectivity enables production teams to review measurements from multiple locations through a unified interface. Historical data can reveal recurring humidity changes associated with equipment operation, ventilation adjustments, seasonal conditions, or maintenance activities. By combining sensor readings with operational information, manufacturers can improve their understanding of environmental behavior and strengthen facility management practices.
Automation can also support more responsive environmental control. When humidity readings approach predefined limits, integrated systems may adjust humidification, dehumidification, or air handling operations according to established control logic. Advanced analytics can identify unusual measurement patterns and help maintenance teams investigate potential sensor drift or equipment problems. However, automated responses must be designed around validated process requirements and appropriate safety controls. Semiconductor manufacturers need dependable communication, secure system access, and reliable fallback procedures to ensure that connected monitoring systems remain effective during operational disruptions.
Challenges in Semiconductor Humidity Monitoring
Despite their benefits, humidity measurement systems face several implementation challenges in semiconductor facilities. Sensors may experience drift, contamination, temperature related errors, or performance changes after prolonged exposure to demanding environments. Differences between sensor technologies can also create measurement inconsistencies when devices are installed without suitable calibration procedures. In addition, poorly selected measurement locations may fail to capture local humidity variations near sensitive equipment or material handling areas. Addressing these issues requires careful system design, appropriate instrument selection, and a structured maintenance program.
Semiconductor manufacturers can improve monitoring reliability by following several practical measures:
- Establish calibration schedules: Verify sensor accuracy at intervals appropriate for the application and manufacturer recommendations.
- Optimize sensor placement:Assess airflow, equipment heat sources, material storage conditions, and localized moisture risks.
- Use suitable instruments:Match the sensing principle and measurement range to the specific process requirements.
- Maintain data quality:Review unusual readings, investigate sensor faults, and document corrective actions.
These practices help manufacturers distinguish genuine environmental changes from measurement errors. A well maintained monitoring network provides more dependable information for quality management and facility optimization.
Role of Humidity Control in Advanced Semiconductor Packaging
Advanced semiconductor packaging introduces additional requirements for moisture management as manufacturers develop increasingly compact and sophisticated electronic assemblies. Packaging materials, substrates, adhesives, and encapsulation compounds may respond differently to moisture exposure. In some applications, absorbed moisture can contribute to defects during subsequent heating or assembly operations. Appropriate humidity monitoring helps manufacturing teams manage storage and production environments according to material specifications. It also supports better handling practices for moisture sensitive components throughout the packaging process.
Humidity sensor technologies can contribute to monitoring storage cabinets, controlled production rooms, component handling areas, and selected assembly environments. Their readings help operators verify whether conditions remain suitable for sensitive materials before processing begins. However, environmental humidity monitoring is not a substitute for material specific moisture testing or prescribed component storage procedures. Manufacturers must combine sensor data with established handling requirements, packaging controls, and quality assurance processes. This integrated approach helps reduce avoidable moisture related risks while supporting consistent assembly quality.
Future Trends in Humidity Sensor Technologies
Future developments are expected to focus on improved sensor stability, smaller device designs, digital connectivity, and more sophisticated data analysis. Advances in sensing materials may improve measurement performance under demanding industrial conditions, while enhanced electronics can support faster response and better compensation for environmental influences. Wireless monitoring may also expand in selected applications where installation flexibility is important. However, wireless systems must meet facility requirements for reliability, cybersecurity, interference management, and maintenance access before being deployed in critical production areas.
Artificial intelligence and predictive analytics may further strengthen environmental monitoring by analyzing historical humidity patterns alongside temperature, airflow, equipment status, and production data. These tools could help identify unusual conditions, estimate the likelihood of environmental excursions, and support preventive maintenance planning. Adoption will depend on data quality, model validation, system integration, and measurable operational benefits. As semiconductor manufacturing becomes more automated, humidity sensor technologies are likely to remain an important part of intelligent facility management and process monitoring strategies.
Conclusion
Precise moisture management is essential for semiconductor manufacturing because sensitive materials, controlled production environments, and advanced assembly processes can be affected by humidity fluctuations. Advanced humidity sensor technologies help manufacturers monitor environmental conditions continuously, detect deviations, and improve the consistency of facility operations. Capacitive sensors, chilled mirror instruments, and specialized moisture analyzers each serve different measurement requirements across cleanrooms, storage areas, and process gas systems. Selecting appropriate technologies and maintaining reliable calibration practices are important for achieving dependable results.
As semiconductor production evolves, integration with smart factory platforms, automated environmental controls, and predictive analytics will create additional opportunities to improve moisture management. Manufacturers that combine suitable sensors with effective maintenance, data monitoring, and process specific controls can strengthen environmental visibility and reduce avoidable operational risks. Ultimately, humidity sensor technologies provide an important foundation for maintaining controlled manufacturing conditions, protecting sensitive materials, and supporting the quality expectations of increasingly advanced semiconductor devices.
Frequently Asked Questions
1. What are humidity sensor technologies in semiconductor manufacturing?
Humidity sensor technologies are measurement methods and devices used to detect moisture levels in air and controlled industrial environments. They help semiconductor manufacturers monitor cleanrooms, storage areas, equipment enclosures, and selected process environments where moisture conditions can influence materials or production quality.
2. Why is humidity control important in semiconductor fabrication?
Humidity control helps maintain stable manufacturing conditions, manage electrostatic discharge risks, and protect moisture sensitive materials. Excessive or insufficient moisture can affect selected materials and processes, making reliable environmental monitoring an important part of semiconductor quality management.
3. Which humidity sensors are commonly used in semiconductor facilities?
Capacitive sensors are commonly used for general relative humidity monitoring. Resistive sensors can support selected industrial applications, while chilled mirror hygrometers and specialized moisture analyzers are suitable for applications requiring highly accurate dew point measurements or trace moisture analysis.
4. How do humidity sensors improve semiconductor cleanroom performance?
Humidity sensors provide continuous measurements that help facility operators identify environmental deviations, evaluate humidity variations across different zones, and manage humidification or dehumidification systems. Integrated monitoring can also generate alerts and preserve historical records for quality investigations.
5. Can humidity sensor technologies reduce semiconductor manufacturing defects?
Reliable humidity monitoring can help reduce certain moisture related risks by identifying environmental conditions that may affect sensitive materials or processes. However, sensors cannot eliminate every defect, and their effectiveness depends on suitable instrument selection, calibration, process controls, and correct interpretation of measurements.
6. How does smart factory automation use humidity sensors?
Smart factory systems collect humidity readings through connected sensors and display them on centralized monitoring platforms. Depending on system configuration, these readings can trigger alerts, support automated environmental adjustments, and provide historical data for predictive maintenance and operational analysis.
7. What factors should manufacturers consider when selecting humidity sensors?
Important considerations include measurement accuracy, response time, operating range, temperature compensation, chemical compatibility, calibration requirements, maintenance needs, communication interfaces, and total ownership cost. The selected instrument should match the environmental conditions and measurement objectives of the specific application.
8. What is the future of humidity sensor technologies in semiconductor manufacturing?
Future developments may include more stable sensing materials, improved digital connectivity, wireless monitoring in suitable applications, and AI enabled analysis of environmental data. These capabilities could improve anomaly detection, maintenance planning, and coordination between environmental monitoring and automated manufacturing systems.
80% of the Forbes Global 2000 B2B companies rely on MarketsandMarkets to identify growth opportunities in emerging technologies and use cases that will have a positive revenue impact.
- Food Packaging Market Size Set for Strong Growth Through 2030 Amid Rising Demand for Convenience Foods
- Crop Protection Chemical Market Size, Share & Growth Forecast (2025–2030)
- Mulch Films Market: Driving Sustainable Agriculture Through Innovation
- Agricultural Adjuvants Market Analysis, Trends, and Growth Outlook (2026–2031)
- Japan Enterprise Asset Management Market Growth: AI and Smart Infrastructure Drive Demand